01 / SLS
Complex geometry. Functional results.
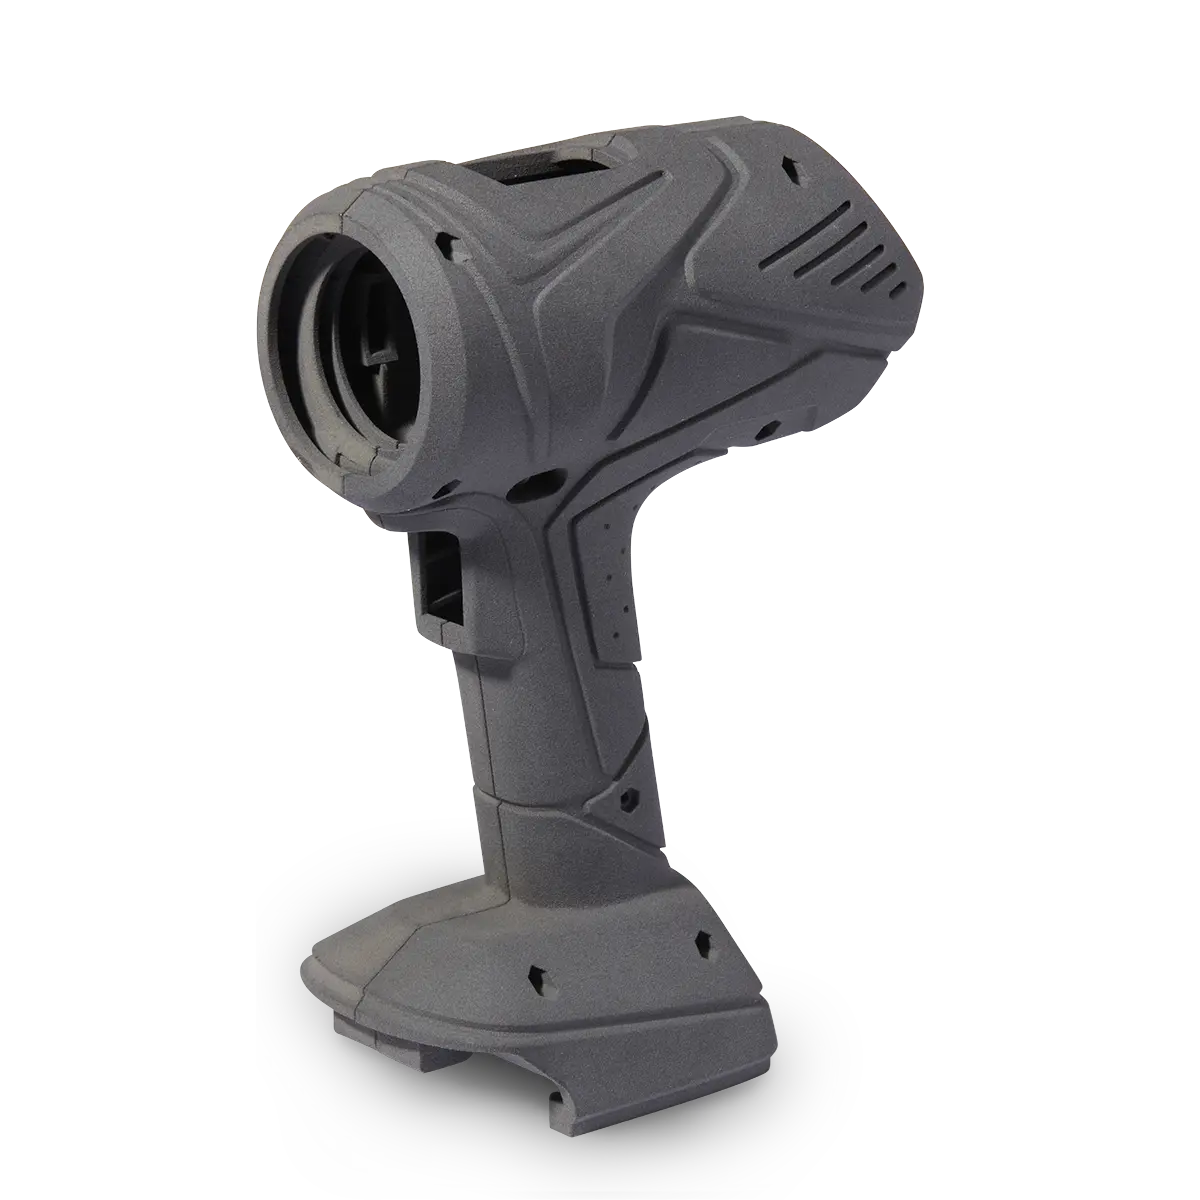
BG 3D PRINT offers SLS 3D printing in Sofia with seven polymer powders — from versatile Nylon 12 to reinforced Nylon 11 CF and Nylon 12 GF and flexible TPU 90A. In selective laser sintering, a laser bonds particles layer by layer while the surrounding powder supports the part. No separate support structures are printed. The process suits functional prototypes, housings, fixtures and small batches with complex geometry. Our calculator estimates cost from the STL model volume, selected material density and quantity. The final quotation is confirmed after review, before production. Material selection should follow the mechanical requirements of your specific application.
- 7
- Engineering powders
- 110 µm
- Layer height
- 165 × 165 × 300 mm
- Fuse 1+ 30W chamber
- €50.00
- Minimum / distinct powder
How powder becomes a part
SLS — Selective Laser Sintering — fuses polymer powder with a laser. It is neither filament extrusion nor the curing of liquid resin.
Prepare
The STL is checked for dimensions, geometry and material suitability. Build placement is chosen for production.
Spread
A thin layer of polymer powder is spread across the build area. Our SLS layer setting is 110 µm.
Sinter
The laser sinters the part cross-section. The platform lowers and the process repeats for the next layer.
Cool
The chamber and parts cool before removal. Cooling is part of manufacturing, not a shipping estimate.
Depowder
Parts are separated from the surrounding powder. Cavities and channels must allow powder removal.
110 µm is the layer height, not a guaranteed dimensional tolerance. ‘100%’ in the calculator means a solid model without an infill selector — not zero microporosity or guaranteed watertightness.
 PA12 / 03—07Most selected